Explainer: Thread Form Differences in Metric Bolts
Metric bolt threads vary in form, pitch, and standard design. These differences determine interchangeability and fit. Procurement teams must verify thread form before purchase to prevent costly assembly failures, rework, and supply delays.
- Metric thread form determines how a bolt fits a nut or threaded insert, so it must be verified during sourcing.
- Coarse and fine pitch metric threads are not always interchangeable even when nominal diameter is the same.
- Procurement teams should require thread form documentation to avoid assembly failures and rework.
- Mixing thread forms in a single assembly creates fit issues and can damage fasteners.
- A worked example shows how a missing thread form note caused a delay during an industrial assembly.
What metric bolt threads actually mean in practice
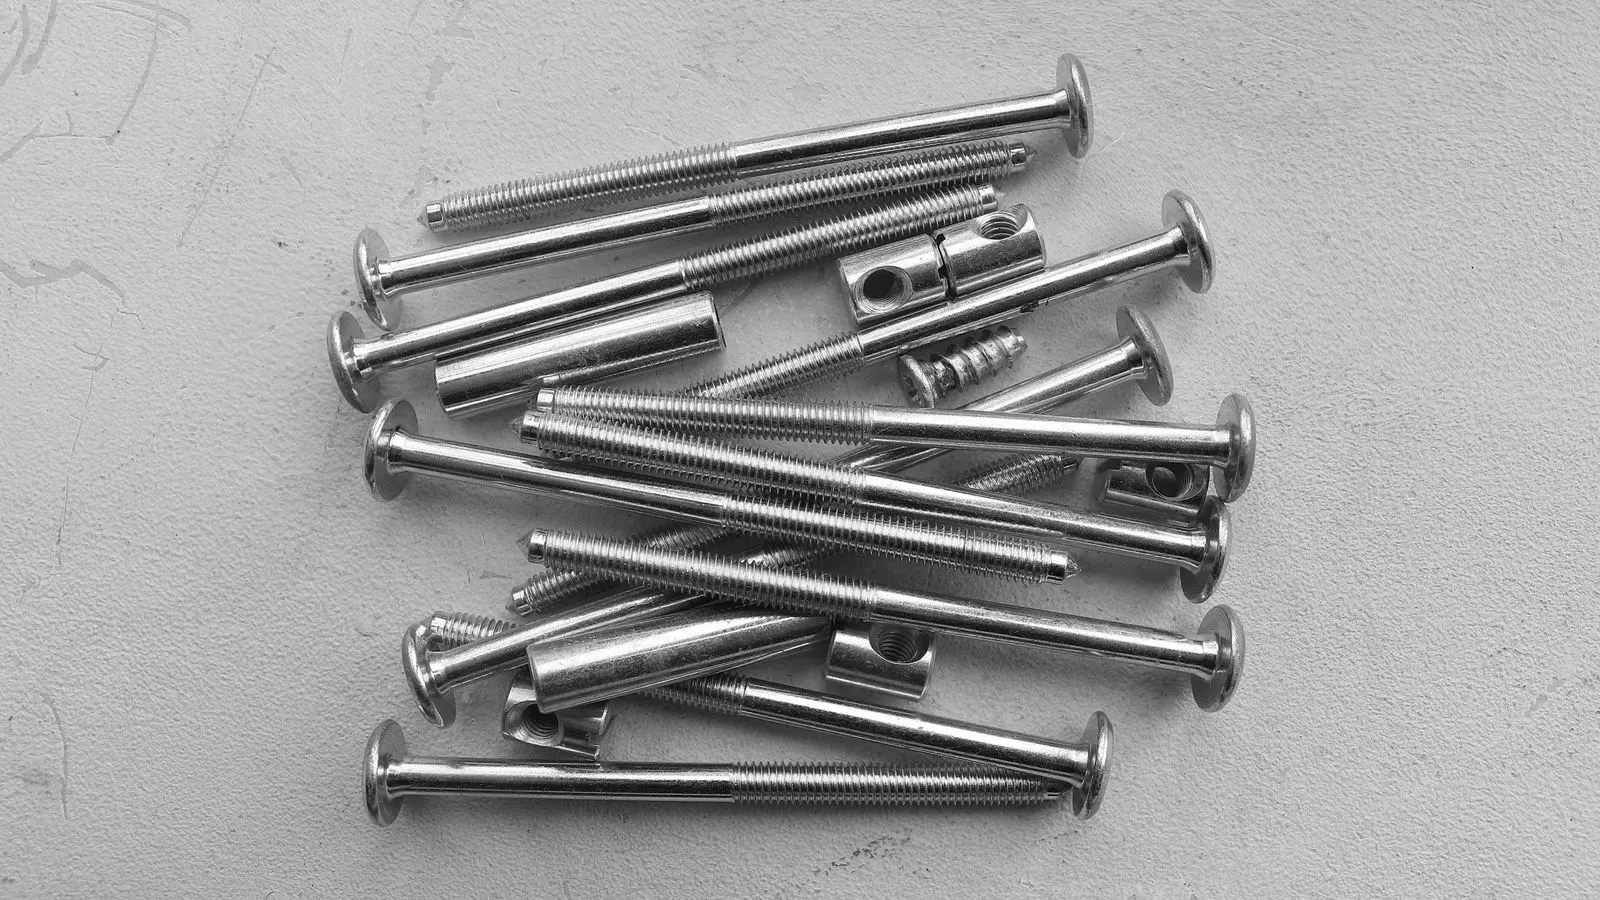
Metric bolt threads are standardized helical profiles used on bolts, nuts, and threaded inserts. The “metric” label refers to the measurement system, but the thread form is what determines physical compatibility. Two bolts may share the same nominal diameter yet behave differently because their thread forms are not identical.
A thread form includes the thread profile angle, the pitch, and the standard it follows. The profile angle is the angle of the thread flank. The pitch is the distance between adjacent thread crests. The standard defines the nominal diameter, pitch, and tolerance class. Procurement teams must check all three when specifying fasteners.
In industrial sourcing, the same nominal size can hide multiple thread forms. A M10 bolt might have a coarse thread, a fine thread, or a special metric thread depending on the application. If a buyer orders only by diameter, the supplier may deliver a thread form that does not match the mating part. This is the most common cause of fit problems on the shop floor.
How thread form affects interchangeability
Interchangeability means that a bolt, nut, or insert from one batch can be used with a mating part from another batch without special tools or adjustment. For metric fasteners, interchangeability depends on matching thread form.
Two fasteners can have the same nominal diameter and still fail to thread together. The thread flanks may be too close, too far, or at the wrong angle. The result is cross-threading, binding, or inability to assemble. In some cases, the parts look correct to the eye but do not mesh properly under load.
Coarse and fine pitch metric threads are a common source of confusion. Coarse threads have a larger pitch and are used for general purpose applications. Fine threads have a smaller pitch and are used where a more gradual thread engagement is needed. A fine thread may have more thread engagement per unit length, but it is not a drop-in replacement for a coarse thread. The nut or insert must match the pitch exactly.
A practical rule is that thread form is a hard requirement, not a preference. If the drawing or specification calls for a coarse thread, a fine thread will not work. If the mating part is a threaded insert, the insert pitch must match the bolt pitch. Procurement teams should treat thread form the same way they treat material grade and surface treatment.
Common thread forms in metric bolt sourcing
Metric thread forms are defined by international standards, but the exact designation varies by region and industry. The most common forms in general purpose industrial work are coarse thread, fine thread, and special metric thread.
Coarse thread is the default for many metric bolts when no other thread form is specified. It is used in general purpose assemblies, structural connections, and many machine components. The pitch is larger, so assembly is faster and the thread is more tolerant of minor surface imperfections.
Fine thread is used where a smaller pitch is required. It is common in precision assemblies, high strength connections, and applications where a gradual thread engagement is preferred. Fine thread can be harder to assemble if the threads are damaged or if the mating part is not clean.
Special metric thread is used in specific industrial contexts, such as certain automotive, aerospace, or heavy equipment applications. These thread forms are not interchangeable with standard coarse or fine metric threads. They are identified by a specific designation and must be ordered as a matched set.
The table below summarizes the common thread forms and their typical sourcing considerations.
| Thread form | Typical use | Interchangeability note |
|---|---|---|
| Coarse metric thread | General purpose assemblies, structural connections | Default when no thread form is specified |
| Fine metric thread | Precision assemblies, high strength connections | Not interchangeable with coarse thread of same diameter |
| Special metric thread | Automotive, aerospace, heavy equipment | Not interchangeable with standard coarse or fine metric |
| Unified thread | Some legacy and mixed systems | Not a metric thread form, requires separate verification |
How thread form affects sourcing decisions
Thread form changes the sourcing workflow in three ways. It affects the part number, the verification process, and the risk of receiving the wrong item.
Part number specificity matters. If the supplier part number does not include the thread form, the buyer is relying on the supplier to infer the correct form. This is risky. A part number that says M10 is not enough. The buyer should require the thread form in the part number or in the purchase order.
Verification requires more than a visual check. A visual check can confirm the diameter, but it cannot confirm the pitch or the profile angle without the right tools. The buyer should require a thread gauge or a thread pitch gauge to verify the received fasteners. For high risk assemblies, the buyer should require a certificate of conformance that states the thread form.
Risk of receiving the wrong item is real. If a buyer orders M10 coarse thread but the supplier ships M10 fine thread, the problem will not be obvious until assembly. The nut or insert will not thread correctly. The result is a line stop, a rework order, or a replacement shipment. Procurement teams should build thread form into the receiving inspection checklist.
A worked example in plain words
A procurement team was sourcing M8 bolts for a machine assembly. The drawing showed M8 bolts but did not state the thread form. The buyer assumed coarse thread because it was the default. The supplier confirmed the order and shipped the bolts.
At the assembly station, the bolts did not thread into the mating nuts. The team checked the bolts and found they had a fine thread. The nuts were coarse thread. The two did not match. The team had to return the bolts and re-order the correct thread form. The delay cost the line a shift.
The fix was simple. The buyer added the thread form to the purchase order. The supplier confirmed the thread form in the part number. The receiving inspector used a thread pitch gauge to verify the shipment. The problem did not repeat.
This example shows that thread form is not a minor detail. It is a critical part of the sourcing chain. When it is missing from the specification, the buyer takes on the risk of a fit failure.
How to verify thread form before purchase
Verification should happen at three points. The first is during specification. The buyer should require the thread form in the drawing or specification. If the drawing does not state it, the buyer should ask the supplier to confirm the default thread form in writing.
The second is during receiving. The buyer should inspect a sample of the received fasteners with a thread pitch gauge. The gauge should match the expected pitch. If the gauge does not fit, the shipment is rejected. For high risk assemblies, the buyer should require a certificate of conformance.
The third is during assembly. The first bolt should be tested in the mating part before the full run. If the first bolt threads smoothly, the rest of the lot is likely correct. If it binds or cross-threads, the lot should be held.
A short checklist helps. The buyer should confirm the nominal diameter, the thread form, and the pitch. The buyer should confirm the standard and the tolerance class. The buyer should confirm the supplier part number matches the specification. The buyer should confirm the receiving inspection includes a thread gauge check.
Common mistakes that cause fit problems
The most common mistake is assuming that the same nominal diameter means the same thread form. This is not true. A M12 coarse thread bolt and a M12 fine thread bolt are not interchangeable.
Another mistake is relying on the supplier to guess the thread form. If the purchase order does not state the thread form, the supplier may ship the default. The default may not match the mating part.
A third mistake is skipping the receiving inspection. The buyer may assume the supplier is correct and skip the thread gauge check. This risk is transferred to the shop floor, where the problem becomes expensive.
A fourth mistake is mixing thread forms in a single assembly. If a bolt, nut, and insert do not all match, the assembly will not work. The buyer should require a matched set for critical assemblies.
These mistakes are avoidable. They are caused by incomplete specifications, weak receiving controls, and a lack of understanding of thread form. Addressing them is a matter of process, not complexity.
How thread form fits with other bolt specifications
Thread form is one part of a larger specification. It works with material grade, surface treatment, and tolerance class. A bolt may be made of high yield steel, zinc plated, and have a fine thread. Each of these attributes affects performance and sourcing.
Material grade determines the strength of the bolt. Surface treatment determines corrosion resistance and lubricity. Tolerance class determines the fit between the threads. Thread form determines the basic geometry. All four must be verified together.
Procurement teams should treat the specification as a complete package. If one attribute is missing, the risk increases. If the thread form is missing, the risk is immediate because the part may not fit. If the material grade is missing, the risk is delayed because the part may fail under load.
The best sourcing practice is to require a complete specification on every purchase order. The supplier should confirm each attribute in writing. The receiving inspector should verify each attribute at the dock. This reduces the chance of receiving a fastener that looks correct but does not perform.
Final notes for procurement teams
Thread form is a core part of metric bolt sourcing. It determines fit, interchangeability, and assembly success. Procurement teams should treat it with the same seriousness as material grade and surface treatment.
The practical steps are clear. Require the thread form in the specification. Require the supplier to confirm it in the part number. Require a thread gauge check at receiving. Require a matched set for critical assemblies. These steps are simple, but they prevent the most common and costly fit problems in industrial fastener sourcing.
When thread form is handled correctly, the sourcing process becomes more reliable. Parts arrive as specified. Assembly runs without delays. The shop floor does not have to diagnose a mismatch that should have been caught before the parts reached the line.
Frequently asked questions
Can I use a coarse metric bolt with a fine metric nut if they are the same diameter?
No. Coarse and fine metric threads are not interchangeable even when the nominal diameter is the same. The pitch must match for the threads to engage properly.
How do I know which thread form a supplier will ship if I only specify the diameter?
You cannot be sure. The supplier may ship a default thread form. You should specify the thread form in the purchase order and require written confirmation before shipment.
What is the fastest way to verify thread form at receiving?
Use a thread pitch gauge that matches the expected pitch. If the gauge does not fit the thread, the fastener does not match the specification.
Does thread form matter for threaded inserts?
Yes. The insert pitch must match the bolt pitch. If the insert is fine thread and the bolt is coarse thread, the bolt will not thread into the insert correctly.
Is there a thread form I should assume if the drawing does not state one?
Coarse thread is often the default for general purpose metric bolts, but you should not assume it. You should require the supplier to confirm the thread form in writing before ordering.