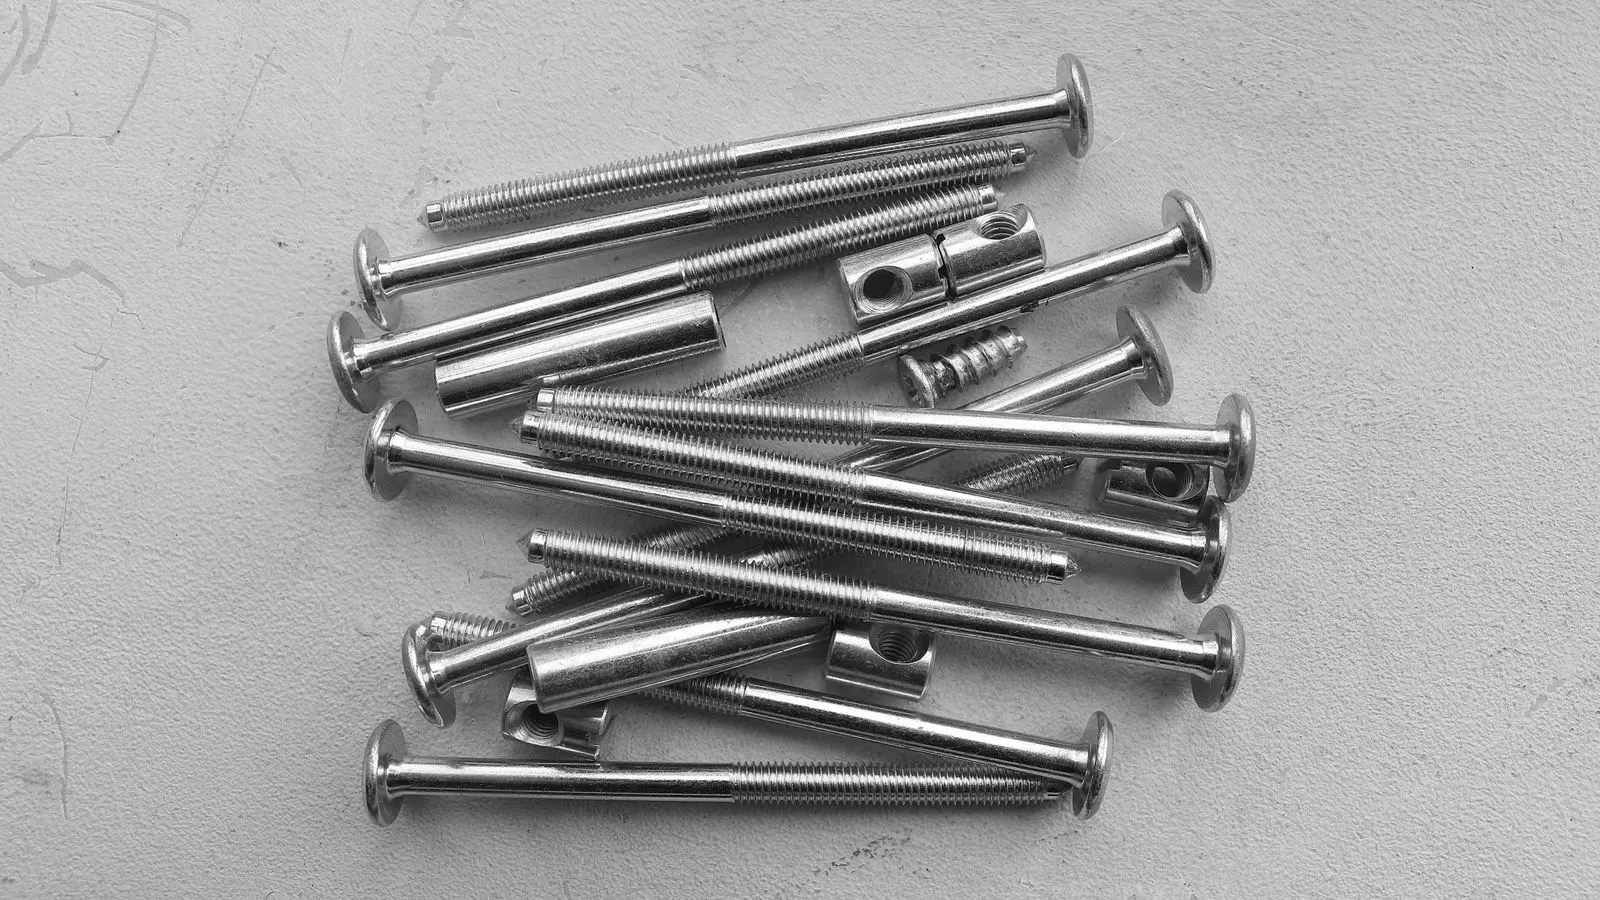
How to Select Grade 10.9 Bolts for High-Load Joints
Choose grade 10.9 bolts by verifying load calculations, material compatibility, and surface finish. This guide provides a step-by-step method for engineers to select the correct high-strength fastener for structural applications.
- Verify material properties against calculated loads before specifying grade 10.9 bolts.
- Account for surface finish and coating when determining final torque values.
- Check thread engagement length to ensure the joint meets design safety factors.
- Confirm heat treatment certification for every batch of high-strength hardware.
Why Grade 10.9 is the Standard for High Load Joints
Grade 10.9 fasteners dominate applications where failure is unacceptable and weight or cost efficiency matters. These bolts offer a balance between high yield strength and manageable fabrication costs. However, selecting the right grade is not about picking the highest number available. It is about matching the material properties to the specific stress profile of the joint. Engineers often default to higher grades without checking if the application actually requires them. This guide walks through the practical method for grade 10.9 bolt selection.
The selection process starts with the load path. If the joint sees fluctuating loads or high vibration, you need to consider fatigue limits, not just static yield. If the joint is in a corrosive environment, the coating choice will alter the effective strength. The goal is to define the exact requirements before looking at a fastener catalog.
Prerequisites: Defining the Engineering Requirements
Before you specify a single bolt, you need a complete set of data. This data set is your prerequisite package. It must include the maximum static load, the dynamic load factor, the joint stiffness, and the material compatibility of the mating parts.
Start with the load calculation. Determine the worst-case static load in kilonewtons or pounds. Apply the appropriate dynamic factor based on the service conditions. For structural connections, this might be a static service, but for machinery, it could be a cyclic fatigue scenario. The distinction changes the entire selection logic. If you are dealing with a static structural joint, you are looking at yield strength. If you are dealing with a machinery joint, you are looking at fatigue limit and proof load.
Next, define the joint geometry. You need the nominal diameter of the bolt, the number of bolts in the joint, and the thickness of the clamped assembly. The thread engagement length is often the most overlooked variable. If you only have one thread pitch, you have a limit. If you have a coarser thread, you have more engagement per inch. This directly impacts the shear and tensile capacity of the fastener.
Finally, check the material of the parts being joined. You cannot specify a high-strength bolt if the base material will yield first. A grade 10.9 bolt in a soft aluminum joint will stretch the bolt before it fails, but it will also stretch the aluminum joint. You must match the strength of the fastener to the strength of the mating parts.
Step 1: Calculate the Required Tensile Strength
The first step in grade 10.9 bolt selection is determining the minimum tensile strength required for the joint. This is not a guess. It is a calculation based on the ultimate load and the safety factor.
Use the calculated load from your prerequisite package. Divide this load by the number of bolts in the joint. This gives you the load per bolt. Then, apply the design safety factor. For structural applications, this factor is often higher than for general machinery. The result is the required minimum proof load per bolt.
Compare this required proof load against the standard values for grade 10.9. Grade 10.9 bolts have a characteristic tensile strength of 1000 MPa and a characteristic yield strength of 900 MPa. However, the proof load is the governing parameter. For smaller diameters, the proof load is slightly higher due to size effects. For larger diameters, it is lower. You must check the specific standard for the diameter you are selecting. If the required proof load exceeds the grade 10.9 capacity, you must move to a higher grade or increase the bolt diameter.
Step 2: Determine the Bolt Diameter and Thread Type
Once you have the required proof load, you select the diameter. This step involves a trade-off between strength and space. A larger diameter bolt provides more strength but requires a larger clearance hole. In dense assemblies, this can be a limiting factor.
Check the thread engagement length. The standard minimum engagement is usually one thread pitch per 10 mm of bolt diameter, or a specific minimum length like 20 mm. If the joint is thin, you may not have enough engagement. In this case, you might need a longer bolt or a coarser thread. A coarser thread increases the engagement per revolution, which is beneficial for short joints.
Consider the thread type. Fine threads provide more engagement per length, which is good for thin plates. Coarse threads are stronger in shear and easier to manufacture. For high-load joints, fine threads are often preferred for their higher tensile capacity, but they are more sensitive to misalignment. If the joint will experience vibration, a coarser thread might hold better because it is less likely to back off.
Step 3: Assess Surface Finish and Coating
The surface finish of a grade 10.9 bolt affects its strength and corrosion resistance. Zinc plating is common, but it is a thin layer. It does not protect against the underlying steel if the plating is damaged. Hot-dip galvanizing is thicker but can be inconsistent in thickness.
For high-load joints, the coating choice impacts the torque. A coated bolt has a different friction coefficient than an uncoated bolt. If you specify a zinc-plated bolt but calculate torque for an uncoated bolt, you will under-torque the joint. Under-torquing is a major cause of fatigue failure. You must specify the coating in your selection process.
Consider the environment. If the joint is in a marine or chemical environment, zinc plating may not be enough. You might need a higher-quality coating or a different material. However, changing the material changes the grade. You are no longer selecting a grade 10.9 steel bolt. You are selecting a stainless steel bolt with different properties. Stick to the steel grade if the environment allows it.
Step 4: Verify Heat Treatment and Certification
Every batch of grade 10.9 bolts must be heat treated. The heat treatment process determines the final strength. Without proper heat treatment, the bolt will not meet the grade specification.
Require heat treatment certificates from the supplier. These documents show the furnace temperature, the quenching medium, and the tempering temperature. They also show the tensile test results. If the supplier cannot provide these documents, do not buy the bolts. This is a non-negotiable step for high-load applications.
Check for proof load testing. The supplier should test a sample of the batch. The test result must be above the minimum proof load. If the result is below the minimum, the batch is rejected. This step ensures that the material properties are consistent across the batch.
Step 5: Match the Bolt to the Mating Parts
The bolt is only as good as the joint it clamps. If the base metal is too soft, the bolt will not perform as expected. The bearing area of the bolt head and nut must be checked against the compressive strength of the base metal.
Calculate the bearing stress. Divide the bolt load by the bearing area. Compare this stress to the allowable bearing stress of the base metal. If the bearing stress is too high, the base metal will deform. This deformation will reduce the clamping force over time.
Check the edge distance. The distance from the bolt center to the edge of the plate must be sufficient. If the edge distance is too small, the plate will tear out under load. Increase the edge distance or use a larger plate thickness.
Step 6: Define the Torque and Tension Specification
The final step in selection is defining how the bolt will be tightened. You cannot just specify the bolt. You must specify the tightening method.
Use the torque method or the direct tension method. The torque method is common because it is easy to apply with a standard wrench. However, it is sensitive to friction. The direct tension method uses a torque wrench or a tension tool to pull the bolt to a specific force. It is more accurate and less sensitive to surface conditions.
For high-load joints, direct tension is preferred. It ensures that every bolt reaches the same tension. This is critical for structural integrity. If you use the torque method, you must specify the lubrication. A dry bolt and a greased bolt will have different torque values for the same tension.
Common Mistakes in Grade 10.9 Selection
Engineers make several common mistakes when selecting high-strength bolts. The first is assuming that a higher grade is always better. A grade 12.9 bolt is stronger, but it is more brittle. It is harder to work with and may crack if not handled carefully. Use the minimum grade that meets the requirements.
The second mistake is ignoring the coating. A zinc-plated grade 10.9 bolt has a different friction coefficient than a plain grade 10.9 bolt. If you calculate torque for one and specify the other, you will have a problem. Always specify the coating.
The third mistake is not checking the thread engagement. If the bolt is too short, it will not have enough threads in the nut. This will cause the threads to shear before the shank yields. Measure the joint thickness and ensure the bolt length provides the required engagement.
The fourth mistake is mixing grades. Do not use a grade 10.9 bolt with a grade 8.8 nut. The nut will fail first. Match the grades of the bolt and the nut.
Final Verification and Documentation
The last step is verification. Before production, review the entire selection. Check the load calculations against the bolt properties. Check the joint geometry against the bolt dimensions. Check the coating and heat treatment certificates.
Create a fastener specification document. This document should list the bolt grade, diameter, length, thread type, coating, and heat treatment requirements. It should also specify the tightening method and the torque or tension value. This document is your reference. It ensures that the right bolts are ordered and installed.
Do not rely on memory. Write it down. A clear specification prevents errors. It also provides a record for future maintenance. If the joint fails, you can trace the error back to the specification.
Conclusion
Selecting the right grade 10.9 bolt is a technical process. It requires careful calculation and attention to detail. By following these steps, you can ensure that your high-load joints are safe and reliable. The key is to match the bolt properties to the specific requirements of the joint. Do not guess. Calculate. Verify. Document.
Frequently asked questions
Can I use grade 10.9 bolts with grade 8.8 nuts?
No. The nut will fail before the bolt because it has lower strength. Always match the grades of the bolt and the nut to ensure the joint fails at the intended strength.
What is the difference between proof load and yield strength?
Proof load is the stress at which the bolt deforms permanently. Yield strength is the stress at which the material begins to deform plastically. For design, you use the proof load as the governing value.
Do I need to lubricate the threads?
Yes. Lubrication reduces friction and allows you to achieve the correct tension with a lower torque value. It also makes installation easier and reduces the risk of over-torquing.
How do I check if a bolt is truly grade 10.9?
Require heat treatment and tensile test certificates from the supplier. You can also use a hardness test, but hardness is not a direct measure of strength. The certificates are the definitive proof.
What happens if I under-torque a grade 10.9 bolt?
The joint will not have enough clamping force. This can lead to vibration, loosening, and fatigue failure. Under-torquing is a common cause of bolt failure in high-load applications.