Fixing Thread Damage Found During Inspection
Apply a structured thread inspection protocol to sort damaged fasteners. Use thread gauges to measure wear, apply defect triage rules to classify severity, and select rework options for minor damage or reject parts that fail critical tolerance limits.
- Apply thread inspection to separate cosmetic wear from structural failure before accepting or rejecting hardware.
- Use thread gauges to verify that damaged threads still engage correctly and maintain required load paths.
- Define rework options only when the defect is localized and does not compromise the stress concentration zone.
- Document every inspection result to support traceability and prevent recurring defects in future lots.
- Reject fasteners immediately if the damage affects the shank, head, or the primary load-bearing region of the thread.
Thread inspection is the first line of defense against fastener failure. When a quality engineer finds a damaged thread during incoming inspection, the decision is rarely binary. Some defects are cosmetic. Others signal a manufacturing error or a handling mistake. A clear protocol separates these categories and prevents weak parts from entering assembly.
What does thread inspection actually measure?
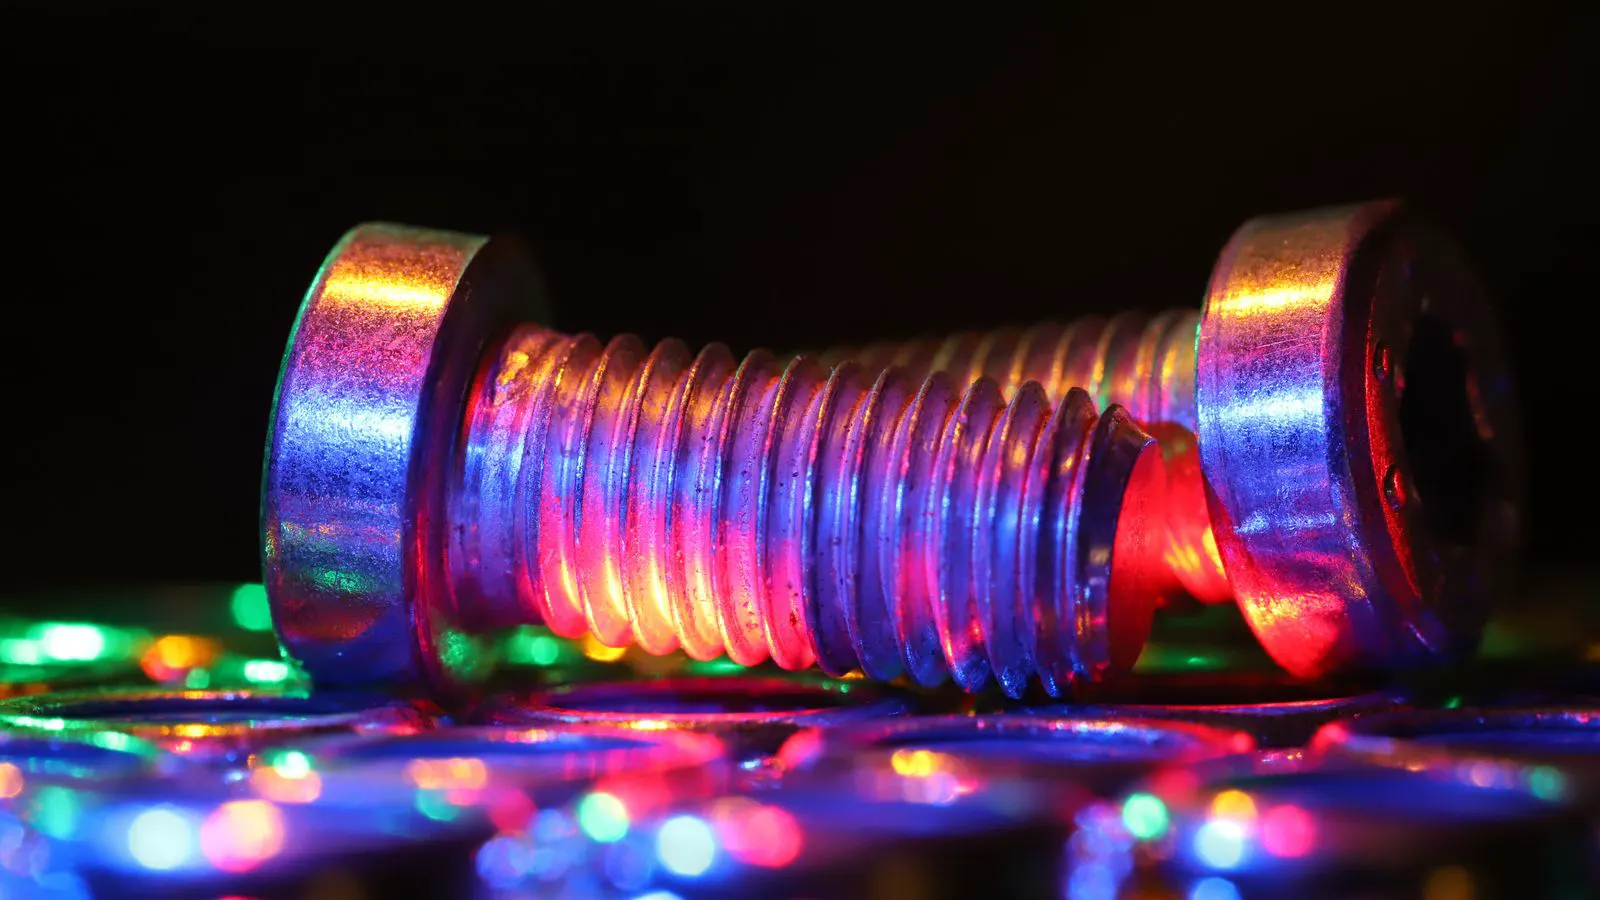
Thread inspection checks three things: geometry, engagement, and surface condition. Geometry confirms that the major and minor diameters match the drawing. Engagement verifies that a mating nut or female thread can still be tightened without cross-threading. Surface condition looks for burrs, nicks, and corrosion that can concentrate stress.
Most thread gauges are plug or ring gauges. They pass through the thread to check for the maximum material limit. If the gauge sticks, the thread is oversized. If it falls out too easily, the thread is undersized or worn. For damaged threads, a gauge test alone is often not enough. The engineer needs a visual check under magnification. A small nick on the crest of a thread can hide until the fastener is under load. A gauge tells you if the thread fits, but it does not tell you if the thread will survive.
The inspection method depends on the part. A hex bolt with a coarse thread is easy to check. A fine-threaded stud in a tight assembly is harder. The engineer must choose a method that can actually see the defect. For large bolts, a simple visual inspection with a good light source and a magnifying loupe is often sufficient. For small screws or self-tapping fasteners, a borescope or a digital microscope may be required to see damage hidden in the threads.
The material of the fastener also changes the inspection focus. Carbon steel fasteners are more susceptible to surface cracks from handling. Stainless steel fasteners are more prone to corrosion pitting. Aluminum fasteners are soft and easily damaged by improper tools. Each material has different failure modes that the inspector must look for.
How to triage thread defects
Defect triage is the step where the inspector decides if the part is good, reworkable, or scrap. The process starts with locating the damage. Is it on the thread, the shank, the head, or the tip? Damage on the thread is the most common. Damage on the shank is usually a manufacturing flaw. Damage on the head can affect clamping force.
The next step is measuring the defect. Use a thread gauge to check if the part still fits within tolerance. Then use a calibrated magnifier to measure the depth of any nick or gouge. If the defect is less than a small fraction of the thread height, it may be acceptable. If it is deeper, the stress concentration increases. The fastener will fail at a lower load.
The triage decision depends on the application. A bolt in a non-critical housing may tolerate more damage than a bolt in a safety-critical joint. The quality engineer must check the drawing and the application notes. If the drawing does not specify, the standard practice is to reject any damage that prevents smooth engagement or exceeds a defined depth limit.
For example, a small scratch on the shoulder of a grade 8.8 hex bolt might be acceptable if the thread itself is intact. However, a scratch on the thread of a grade 8.8 bolt used in a bridge connection is not acceptable. The difference is not in the defect, but in the consequence of failure. The inspector must know the service condition.
Rework options for damaged threads
Rework is only possible for minor defects. If the thread is nicked but still fits the gauge, the engineer can clean and deburr the area. This removes the stress raiser. If the thread is slightly undersized, the part may be rejected. Reworking a thread to make it larger is not a standard practice. It changes the fit and the load distribution.
If the thread is damaged at the tip, the tip can sometimes be cut off. This is only allowed if the remaining thread length is still sufficient for the design. The drawing usually specifies the required thread engagement. If the rework reduces the engagement below that limit, the part must be rejected.
Rework must be documented. The inspector records the defect, the rework performed, and the final inspection result. This keeps the traceability chain intact. If a fastener is reworked, it is no longer a new part. It is a repaired part. The records must reflect that.
Deburring is the most common form of rework. It involves using a small file, a wire brush, or a deburring tool to remove sharp edges from the thread crests. This must be done carefully. The tool must not remove too much material. If the tool cuts into the thread root, it creates a new stress concentration. The rework must be inspected again to ensure it did not make the problem worse.
For threaded inserts, rework is almost never an option. If the internal thread of a brass or steel insert is damaged, the insert is usually discarded. Attempting to repair an insert often compromises its shear strength.
When to reject fasteners immediately
Some defects are not worth rework. Reject the part if the damage affects the shank. A crack or a large gouge in the shank means the fastener will fail under tension. Reject the part if the head is damaged. A cracked head or a deformed head will not hold the bolt in place. Reject the part if the thread is stripped. A stripped thread cannot hold a nut. It will not clamp.
Reject the part if the gauge test fails and the defect is large. If the thread is worn smooth, it will not hold. If the thread is pitted, the pitting will grow under load. These are structural failures. Do not try to save them.
The rejection process must be clear. Mark the part as rejected. Remove it from the stock. Record the reason. This data helps the supplier or the process owner fix the problem. If the same defect appears in multiple lots, the root cause is not random. It is a process issue.
For instance, if a batch of bolts all shows the same type of burr on the head, the cause is likely the same machine or the same operator. The rejection record should note the specific pattern. This allows the quality team to identify the source and implement a fix.
A practical inspection table
Use this table to guide the decision. It covers common symptoms, likely causes, and the correct action.
| Symptom | Likely cause | What to do |
|---|---|---|
| Small nick on the crest | Handling damage or burr from cutting | Clean, deburr, and re-inspect with a gauge |
| Thread is slightly undersized | Incorrect die size or wear | Check the gauge. If within tolerance, accept. If not, reject |
| Thread is oversized | Incorrect die size or burr | Check the gauge. If it does not pass, reject. Do not rework |
| Cracked shank | Manufacturing flaw or overload | Reject immediately. Do not rework |
| Stripped thread | Cross-threading or over-tightening | Reject. Replace the part |
| Corrosion on the thread | Storage or environmental exposure | Clean and inspect. If the thread is smooth, accept. If pitted, reject |
The table is a starting point. The final decision always depends on the specific application and the drawing.
Prevention tips for future lots
Prevention is cheaper than inspection. If the same defect appears repeatedly, fix the process.
- Check the supplier. If a supplier consistently provides parts with nicks, ask for a process improvement. Ask for a deburring step or a better cutting tool.
- Check the storage. Corrosion and damage often happen in storage. Use desiccant bags and clean storage areas.
- Check the handling. Operators can damage threads. Use proper tools. Do not force nuts into place. If a thread does not start easily, stop and check.
- Check the assembly. If threads are damaged during assembly, the problem is in the assembly process. Use torque-controlled tools. Do not use impact drivers on fine threads.
- Check the documentation. If the drawing does not specify the tolerance for thread damage, add it. A clear spec prevents arguments and ensures consistency.
Prevention reduces the need for inspection. It also reduces the risk of failure in the field.
How to document the inspection
Documentation is part of the inspection. Without records, the process is not repeatable. The inspector must record the part number, the lot number, the defect type, the measurement, and the decision.
Use a standard form. It should have fields for the defect location, the gauge used, and the magnification level. It should also have a section for rework. If the part is reworked, record the rework performed and the final inspection result.
The records should be accessible. If a failure happens in the field, the quality team needs to trace the lot back to the inspection records. The records should show what was checked and what was accepted.
Good documentation also helps in supplier management. If a supplier has a high rejection rate, the records show the pattern. The quality engineer can use the data to negotiate improvements or switch suppliers.
The protocol is simple. Inspect, measure, triage, rework or reject, and document. Follow it every time. It protects the product and protects the process.
Frequently asked questions
Can I accept a bolt with a small nick on the thread?
Yes, if the nick is shallow and does not prevent smooth engagement. Clean and deburr the area, then re-inspect with a thread gauge. If the gauge passes and the nick is within tolerance, the part is acceptable.
What if the thread gauge does not pass?
Reject the part. If the gauge does not fit, the thread is out of tolerance. Do not attempt to rework it. Replace the part.
How do I know if a thread is stripped?
Check if a nut can be tightened by hand. If the nut spins freely or does not engage, the thread is stripped. Reject the part.
Can I rework a thread that is too large?
No. Reworking a thread to make it smaller is not a standard practice. It changes the fit and the load distribution. Reject the part.
How do I prevent thread damage in storage?
Use clean, dry storage areas. Use desiccant bags to control humidity. Handle parts with care to avoid nicks and burrs.