Buyer's Guide to Selecting Self-Tapping Screws
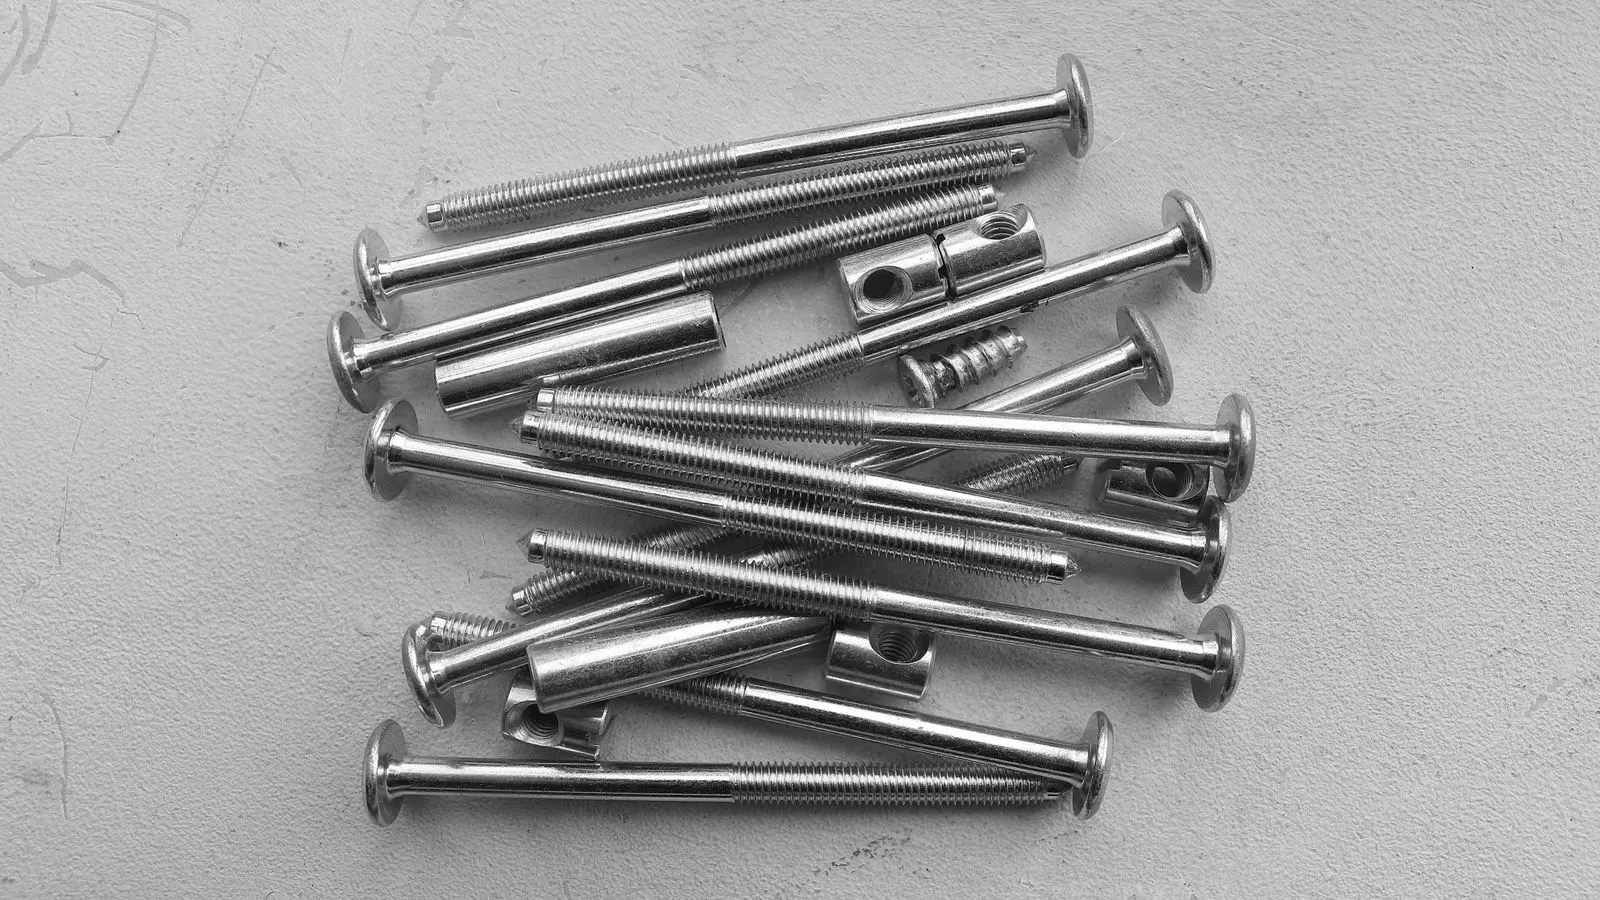
Choose self tapping screws by matching thread form, material, and coating to the workpiece. This guide covers selection criteria for sheet metal and structural applications, helping buyers avoid common installation failures.
- Match the screw thread form to the base material and thickness.
- Select the base metal and coating based on the service environment.
- Verify the pilot hole diameter and depth against the manufacturer's data.
- Check the head style and drive type for the assembly method.
- Review the torque specification and clamp load requirement before ordering.
What is the difference between self tapping screw types
Self tapping screws form a large category of sheet metal fasteners. The term covers screws that cut their own thread into the material. Buyers often confuse these with wood screws or tapping screws.
The core difference lies in the thread form and the material being fastened. A self tapping screw for sheet metal has a sharp, self-piercing tip. It removes a small amount of material as it advances. The thread is usually slightly undercut to create a bearing surface.
There are three main thread forms to consider.
The first is the Phillips or flat head style. This is the most common form for light sheet metal. It is used for aluminum, mild steel, and thin stainless steel. The thread is relatively shallow.
The second is the thread form for thicker materials. These screws have a deeper thread and a stronger point. They are designed for steel plate up to a certain thickness. The thread engages more of the base material cross-section.
The third is the form for high strength applications. These screws use a coarser thread and a stronger base metal. They are often used in automotive or structural sheet metal. The thread form is designed to handle higher shear loads.
When selecting a fastener, the thread form must match the material. Using a shallow thread on thick steel will strip. Using a deep thread on thin aluminum will tear the material. The selection process starts here.
How to match the screw to the base material
The base material dictates the screw specification. This is the first decision point in any sourcing process.
For aluminum and magnesium, the screw must be soft enough to cut cleanly. A hardened steel screw can shatter the aluminum edge. The thread form should be designed for these softer metals. The tip must be sharp. The thread should be slightly undercut to allow the material to flow.
For mild steel, the screw must be harder than the base material. The point needs to pierce the steel and cut a clean thread. The thread form is typically deeper than for aluminum. The steel sheet must have a minimum thickness to hold the thread.
For stainless steel, the material is harder than mild steel. The screw point needs to be very sharp. The thread form must be strong. The stainless sheet also has a different grain structure. This affects how the thread cuts.
The base material also affects the pilot hole. A pilot hole is a small hole drilled before driving the screw. It reduces the force needed. It prevents the material from tearing. The hole diameter depends on the screw thread form and the material thickness.
For aluminum, the pilot hole is larger. For steel, it is smaller. For stainless, it is in between. The manufacturer provides the recommended diameter. This data is critical for assembly.
What thread form should you choose
Thread form selection is a technical step. It involves matching the screw to the material and the load.
The thread pitch determines the number of threads per inch or per centimeter. A finer pitch creates more thread engagement. It provides better holding power. A coarser pitch is easier to cut. It requires less torque.
The thread angle affects the shear strength. A 60 degree thread is stronger than a 30 degree thread. It also requires a different tool for cutting. The angle must match the cutting tool used in the factory.
The thread depth is another factor. A deeper thread engages more of the base material. It provides higher shear strength. However, it requires a thicker material. A shallow thread works for thin sheet. It is easier to install.
The thread form also affects the noise. A fine pitch thread can squeal in high speed assembly. A coarse pitch thread is quieter. The choice depends on the application.
When selecting a screw, check the thread form against the material. Do not guess. Use the manufacturer’s data. The data sheet lists the recommended thread form for each material and thickness.
How to select the base metal and coating
The base metal of the screw determines its strength. The coating determines its corrosion resistance. These are two separate decisions.
For general indoor applications, a steel screw with a zinc coating is common. The steel provides strength. The zinc protects against rust. This is the most economical choice.
For outdoor or marine applications, stainless steel is preferred. The stainless base resists corrosion. It does not need a coating. It is more expensive than steel. It also has lower strength.
For high strength applications, a hardened steel screw is used. The steel is heat treated to increase hardness. It can handle high loads. It must be coated to prevent rust. The coating is usually a thicker zinc layer.
The coating type also affects the color. Zinc is grey. Stainless is silver. A colored coating can be used for identification. The color is not a strength indicator. It is a visual aid.
When selecting a fastener, match the base metal to the load. Match the coating to the environment. Do not mix them. A high strength screw with a weak coating will fail. A low strength screw with a strong coating will shear.
What head style and drive type to use
The head style determines how the screw is driven. The drive type determines the tool used. These must be compatible.
The head style can be a flat head, a countersunk head, or a hex head. A flat head sits on the surface. A countersunk head sits below the surface. A hex head is used with a wrench.
The drive type is the recess in the head. A Phillips drive is common. A Torx drive is more secure. A square drive is for older tools. The drive type must match the tool used in the assembly line.
The head size must match the sheet thickness. A small head on thick steel will not provide enough bearing surface. A large head on thin aluminum will be bulky. The head size is chosen based on the material and the design.
The head style also affects the clamp load. A countersunk head provides a lower profile. It is used when the fastener must be flush with the surface. A flat head provides a higher profile. It is used when the fastener must be visible.
When selecting a screw, check the head style against the assembly method. The tool and the head must work together. A mismatch will strip the drive. It will also reduce the clamp load.
How to verify the pilot hole and torque
The pilot hole and the torque are the final checks. They determine if the screw will hold.
The pilot hole diameter is critical. It must be the right size. If it is too large, the thread will not grip. If it is too small, the screw will strip. The manufacturer provides the recommended diameter. This is based on the thread form and the material thickness.
The pilot hole depth is also important. It should be about half the screw length. It reduces the force needed to cut the thread. It prevents the material from tearing.
The torque is the force applied to the screw. It must be within the manufacturer’s range. Too little torque will not clamp the materials. Too much torque will strip the thread. The torque is measured in Newton meters or inch pounds.
The torque depends on the material, the thread form, and the screw size. The manufacturer provides the recommended torque. This is a critical data point. Do not guess.
When verifying the pilot hole and torque, use the manufacturer’s data. Check the thread form, the material thickness, and the screw size. This ensures the screw will hold. It prevents stripping and breakage.
Sourcing checklist for self tapping screws
The final step is to compile the selection into a purchasing order. This ensures the right part is ordered.
The checklist must include the following items.
- The thread form and pitch.
- The base metal and coating.
- The head style and drive type.
- The pilot hole diameter and depth.
- The torque specification.
- The quantity and packaging.
This list provides a clear specification to the supplier. It reduces the risk of ordering the wrong part. It also speeds up the receiving process.
When reviewing the order, check the data sheet against the checklist. Verify each item. This is the last check before the screws are ordered. It ensures the fastener is correct for the application.
The selection process is a series of decisions. Each decision depends on the previous one. The thread form depends on the material. The base metal depends on the load. The coating depends on the environment. The head style depends on the assembly method. The pilot hole and torque depend on all of these.
When the decisions are made, the selection is complete. The order can be placed. The screws are ready for assembly.
Frequently asked questions
Can I use a self tapping screw on wood?
No, self tapping screws are designed for metal. Wood screws have a different thread form and a different point. Using a self tapping screw on wood will not hold properly.
What is the maximum thickness for a self tapping screw?
It depends on the thread form and the material. Thin sheet metal can use a shallow thread. Thick steel requires a deeper thread. Check the manufacturer's data for the maximum thickness.
Do self tapping screws need a pilot hole?
Yes, a pilot hole is recommended. It reduces the force needed and prevents stripping. The hole diameter depends on the thread form and the material thickness.
Can I use a self tapping screw on stainless steel?
Yes, but the screw point must be sharp and the thread form must be strong. Stainless steel is harder than mild steel. It requires a specific screw type.
How do I know if a self tapping screw is too strong?
It is not usually a problem. A strong screw will hold well. The issue is if it is too weak. It will strip or shear. Match the screw strength to the load.